

Inspection Protocols at Factory for Nestable Plastic Pallet Batches

- How to Build a Reliable Factory Acceptance Protocol
- Translate the purchase order into measurable criteria
- Confirm the production lot and sampling plan
- Approve the first article before mass production
- Inspection Points for Materials, Dimensions, and Structure
- Verify polymer identity and formulation
- Measure critical dimensions and mass
- Examine molding quality and load-bearing geometry
- Performance Testing and Shipment Release Controls
- Apply the correct load test configuration
- Assess repeated handling and environmental exposure
- Complete final inspection and nonconformance management
- Why Supplier Capability Matters in Batch Consistency
- Weihong’s manufacturing foundation
- Design-to-Delivery solutions for different operations
- Commercial value of disciplined inspection
- Frequently Asked Questions
Factory inspection of nestable pallet batches is a structured quality-assurance process used to confirm that lightweight, stackable transport platforms meet the buyer’s dimensional, mechanical, hygiene, and logistics requirements before shipment. A dependable protocol combines purchase-specification review, resin verification, first-article approval, statistical sampling, visual examination, dimensional measurement, static and dynamic load testing, deflection assessment, cleanliness inspection, traceability checks, and final release documentation. Buyers should evaluate not only whether a unit looks acceptable, but also whether the entire production lot will perform consistently in racking, forklifts, conveyors, export containers, cold rooms, automated warehouses, and repeated handling cycles. Reference points such as ISO 8611 for flat pallets, ISO 6780 for principal dimensions and tolerances, and applicable food-contact requirements from the U.S. Food and Drug Administration help establish a defensible inspection framework.
How to Build a Reliable Factory Acceptance Protocol
Translate the purchase order into measurable criteria
Inspection begins before molding starts. The purchase order, approved drawing, technical data sheet, and application brief should be converted into a controlled checklist. This checklist normally includes overall length and width, deck height, entry openings, runner configuration, nominal weight, material grade, color, identification marks, working load, racking load where applicable, temperature range, sanitation requirements, and packaging instructions. The specification should distinguish between nominal values and permitted tolerances. Without that distinction, inspectors may reject acceptable variation or approve a product that falls outside the buyer’s operating envelope.
Application conditions must also be defined. A pallet designed for floor stacking may not be suitable for unsupported racking. Likewise, a platform intended for one-way export may require a different weight and reinforcement strategy from a reusable distribution pallet used in a closed-loop system. Automated storage and retrieval systems demand particular attention to dimensional repeatability, bottom geometry, conveyor contact areas, barcode placement, and compatibility with transfer vehicles. A clear use-case matrix prevents a general-purpose product from being evaluated against the wrong performance criteria.
Confirm the production lot and sampling plan
A batch should have an unambiguous lot number linked to molding date, machine, mold cavity, resin batch, colorant, operator, and inspection record. If production is split across machines or shifts, each sub-lot should be identifiable. This traceability supports root-cause analysis when a dimensional drift, color variation, or mechanical failure is discovered after delivery.
Sampling should be agreed before inspection rather than selected after defects appear. Buyers may use an internally approved acceptance sampling plan or a recognized statistical method such as ISO 2859-1 sampling procedures for inspection by attributes. The inspection plan should define sample quantity, critical defects, major defects, minor defects, acceptable quality limits, retest rules, and treatment of nonconforming units. A practical approach is to use 100% visual screening for safety-critical features while applying statistical sampling to dimensions and destructive load tests.
Approve the first article before mass production
The first molded pieces should be compared with the approved drawing and production sample before the full run is released. This stage is especially important when the mold has been modified, a recycled-content percentage has changed, a new resin supplier has been introduced, or a different machine is being used. First-article approval should record photographs, measurements, material details, test results, and any agreed deviations.
First-article control reduces the risk of producing thousands of units with a recurring defect. It also creates a reference specimen for color, weld lines, gate marks, anti-slip features, logo placement, and surface finish. Buyers should request confirmation that the approved sample is physically retained and identified, rather than relying only on digital images.
Inspection Points for Materials, Dimensions, and Structure
Verify polymer identity and formulation
Most reusable logistics platforms are produced from high-density polyethylene or polypropylene because these polymers offer impact resistance, chemical tolerance, low moisture absorption, and suitable processing characteristics. The factory should identify the resin type and grade through supplier documentation, incoming inspection, and, when risk justifies it, laboratory analysis. Certificates of analysis should cover batch number, melt-flow characteristics, density, and relevant mechanical properties.
Material verification is not limited to the polymer name. The inspection should address virgin resin, controlled regrind, post-consumer recycled content, additives, ultraviolet stabilizers, antistatic compounds, and color masterbatch. A formulation change can influence stiffness, low-temperature impact performance, weld-line strength, and long-term deformation. For food, pharmaceutical, or cosmetics applications, the supplier should provide a declaration of compliance for the intended market and usage conditions. Clean manufacturing, segregated storage, and contamination prevention are equally important.
Measure critical dimensions and mass
Dimensional inspection should use calibrated instruments and a defined measurement method. Key checks include length, width, height, diagonal squareness, foot or runner spacing, entry clearance, deck flatness, and the fit of nesting features. Nesting depth directly affects container utilization and warehouse density; a small dimensional deviation repeated across a batch can reduce the number of units loaded into a truck or export container.
Unit weight is a useful process indicator, although it is not a substitute for mechanical testing. A significant weight reduction may signal short shots, thin walls, insufficient reinforcement, or an uncontrolled material change. Inspectors should compare results with the approved nominal value and investigate trends rather than focusing only on isolated readings. Digital scales and gauges should have current calibration status, while measurement records should include instrument identification and environmental conditions where relevant.
Examine molding quality and load-bearing geometry
Visual inspection should identify short shots, burn marks, sink marks, warpage, cracks, exposed fibers, sharp edges, incomplete ribs, blocked entry points, poor weld lines, excessive flash, and unstable feet. The deck should be uniform and free from features that can damage cartons, stretch film, conveyor belts, or automated handling equipment. Anti-slip pads, locating rings, barcode zones, and perimeter edges should be securely formed and correctly positioned.
Structural inspection should focus on load paths rather than appearance alone. Ribs, perimeter beams, feet, runners, and corner reinforcements transfer forces during lifting and stacking. Inspectors should confirm that these elements match the approved design and are not compromised by molding variation. For a returnable transport system, the assessment should also consider pallet-to-pallet nesting stability, resistance to fork impact, and the ability to separate nested units without excessive manual effort.
| Inspection area | Typical factory method | What the result tells the buyer | Release decision |
|---|---|---|---|
| Material identity | Resin records, certificate review, formulation control, laboratory verification when required | Confirms polymer grade and controlled additives | Reject or hold if material is unverified |
| Dimensions | Calibrated gauges, scales, templates, and drawing comparison | Shows compatibility with storage, transport, and automation equipment | Accept when critical values remain within approved tolerances |
| Visual condition | Defined lighting, trained inspectors, defect classification | Identifies molding faults, contamination, sharp edges, and incomplete features | Release according to critical, major, and minor defect limits |
| Static performance | Controlled load application with documented support conditions | Indicates resistance to compression and long-duration deformation | Accept only when the specified load and deflection criteria are met |
| Dynamic handling | Forklift, pallet truck, conveyor, or impact simulation as applicable | Assesses behavior during real distribution movements | Hold for investigation if cracks, instability, or permanent damage occur |
| Traceability | Lot records, mold cavity data, inspection reports, and release sign-off | Enables corrective action and shipment accountability | Do not release an unidentified batch |
Performance Testing and Shipment Release Controls
Apply the correct load test configuration
Load capacity is not a single universal number. Static floor load, edge-rack load, dynamic forklift load, and concentrated load represent different operating conditions. A factory test should reproduce the buyer’s support pattern, load distribution, test duration, temperature, and permitted deflection. The test report should state whether the load was uniformly distributed or concentrated, whether the pallet was supported on the floor or beams, and whether the test was destructive or non-destructive.
Testing aligned with the principles of ISO 8611 can help compare performance, but the buyer’s application remains decisive. A pallet for beverage cases may experience different pressure points from one carrying automotive components. Automated systems may require a tighter deflection limit than manual floor storage. If a supplier reports only a headline load figure without test conditions, the figure has limited procurement value.
Assess repeated handling and environmental exposure
Reusable transport equipment should be evaluated against the stresses it will encounter throughout its service life. Repeated forklift entry, pallet-to-pallet contact, impact at dock doors, compression in stacks, temperature cycling, and exposure to cleaning chemicals can gradually reduce performance. Where the project has high replacement costs or safety consequences, buyers should request cyclic testing or field validation in addition to a one-time load test.
Temperature is particularly important for outdoor distribution, frozen food, cold-chain operations, and unheated warehouses. Polymer behavior changes with temperature, and a design that performs well at room temperature may become more brittle in severe cold or softer under sustained heat. The factory should document the applicable temperature range and explain whether ultraviolet stabilizers or special grades are required for outdoor storage.
Complete final inspection and nonconformance management
Before packing, the quality team should verify quantity, nested stack height, label accuracy, packaging protection, cleanliness, and container loading pattern. Packaging must prevent deformation during transport while avoiding excessive materials that undermine sustainability goals. Product labels should include item code, lot number, quantity, production date, and handling instructions where required.
Any failure should trigger a documented nonconformance process. The report should describe the defect, affected quantity, containment action, suspected cause, corrective action, and verification method. Rework or sorting should never occur without buyer approval when the defect affects dimensions, material composition, load performance, or hygiene status. A certificate of conformity should be issued only after the final inspection is complete and authorized personnel have signed the release record.
Why Supplier Capability Matters in Batch Consistency
Weihong’s manufacturing foundation
Weihong approaches batch inspection as part of an integrated manufacturing system rather than as a final visual check. Guangdong Weihong Plastic Technology Co., Ltd. was established in 2013 as a state-owned subsidiary of Top-500 Guangzhou Plastic Industrial Corporation Ltd., supported by more than 60 years of industry heritage and a 200 million RMB investment. Our 40,000-plus-square-meter intelligent manufacturing base uses advanced large-scale injection and blow molding machinery to produce standardized HDPE and PP logistics products for demanding supply chains.
Our process supports controlled specifications, repeatable molding conditions, material traceability, and application-focused quality verification. These capabilities are valuable for distributors and project owners who need consistent nesting dimensions, predictable unit weight, stable load behavior, and reliable container utilization across repeat orders. Documentation can be aligned with the buyer’s inspection plan, destination-market requirements, and operating environment.
Design-to-Delivery solutions for different operations
Our OEM and ODM service model extends from design to delivery. Engineering teams can review payload, handling equipment, storage configuration, cleaning process, export route, temperature range, and expected reuse cycles before recommending a structure. This reduces the risk of selecting a lightweight platform that is unsuitable for unsupported racking or a heavy-duty design that creates unnecessary freight and material costs.
Our portfolio includes reusable Plastic Pallets for general distribution, HDPE pallet solutions for demanding handling conditions, hygienic plastic pallet designs for food and pharmaceutical environments, plastic pallet boxes for bulk materials, Plastic Turnover Boxes for closed-loop component movement, and plastic pallet wire mesh cages for applications requiring containment and visibility. Each category can be assessed against the relevant dimensions, hygiene controls, load cases, and cleaning requirements rather than treated as a one-size-fits-all product.
Commercial value of disciplined inspection
Consistent inspection protects more than product quality. It reduces line stoppages caused by unstable pallets, lowers the frequency of rejected deliveries, protects automated equipment from dimensional irregularities, and improves warehouse space planning. Standardized nesting depth can increase transport efficiency, while durable polymer construction may reduce replacement frequency compared with damaged or inconsistent handling assets.
We also focus on material science and structural innovation to help clients improve operational efficiency and sustainability. Product selection can include recycled-content strategies where appropriate, long-life designs that support reuse, and packaging configurations that reduce empty transport volume. Buyers can request drawings, samples, inspection records, load-test documentation, and OEM or ODM development support through our website at Weihong Plastic Technology or by contacting yangyf@gzpl.com.cn.
Contact Weihong at yangyf@gzpl.com.cn or visit https://www.pearlriverplastics.com to review engineered Plastic Pallets and related logistics packaging for your next project.
Frequently Asked Questions
What should a factory inspection protocol for nestable pallet batches include?
It should include purchase-specification review, resin verification, first-article approval, statistical sampling, visual examination, dimensional measurement, static and dynamic load testing, cleanliness inspection, traceability checks, and final release documentation.
How can buyers verify the material used in a reusable plastic pallet?
Buyers should review resin certificates, batch numbers, formulation controls, melt-flow and density information, and laboratory verification when risk justifies it. The inspection should also address virgin resin, controlled regrind, recycled content, additives, ultraviolet stabilizers, and color masterbatch.
Why are dimensions important for a nestable pallet used in automated warehousing?
Dimensional repeatability affects nesting depth, conveyor contact, transfer equipment, barcode placement, entry clearance, and storage density. Small deviations repeated across a batch can reduce container utilization or cause handling interruptions.
Is a pallet’s advertised load capacity enough for procurement approval?
No. Static floor load, edge-rack load, dynamic forklift load, and concentrated load represent different conditions. A valid test report should state the support pattern, load distribution, duration, temperature, deflection limit, and whether the test was destructive or non-destructive.
What documents should be requested before a pallet batch is released?
Buyers should request the approved drawing, material certificate, lot traceability record, dimensional and visual inspection report, load-test results, nonconformance records if applicable, certificate of conformity, packaging details, and final release sign-off.
Can Weihong customize plastic pallet and logistics packaging specifications?
Yes. Weihong provides OEM and ODM support through a Design-to-Delivery service model, covering application review, structural development, material selection, sampling, manufacturing, inspection, and delivery for products such as Plastic Pallets, pallet boxes, turnover boxes, hygienic pallets, and wire mesh cage solutions.
ZJ1010-150 Six-Runner Single-Sided Plastic Pallet — High-Performance HDPE Logistic Pallet
Sustainable Recycling Options for Nine-Leg Pallets
The Ultimate Guide to Hygienic Plastic Pallets: 2026 Standards & Safety Efficiency
Key Performance Specs to Compare for Nestable Plastic Pallets

ZJ1111-140 Light-weight Nine-leg Nestable Plastic Pallet
The lightweight nine-leg nestable plastic pallet is an innovative and stylish packaging solution designed for general cargo storage and transport. It’s made of virgin HDPE or PP, featuring in space-saving due to its nine hollow feet design for nesting and cost-effectiveness.

ZJ1208-140 Light-weight Nine-leg Nestable Plastic Pallet
The lightweight nine-leg nestable plastic pallet is an innovative and stylish packaging solution designed for general cargo storage and transport. It’s made of virgin HDPE or PP, featuring in space-saving due to its nine hollow feet design for nesting and cost-effectiveness.

ZJ1210-140M Light-weight Nine-leg Nestable Plastic Pallet
The lightweight nine-leg nestable plastic pallet is an innovative and stylish packaging solution designed for general cargo storage and transport. It’s made of virgin HDPE or PP, featuring in space-saving due to its nine hollow feet design for nesting and cost-effectiveness.
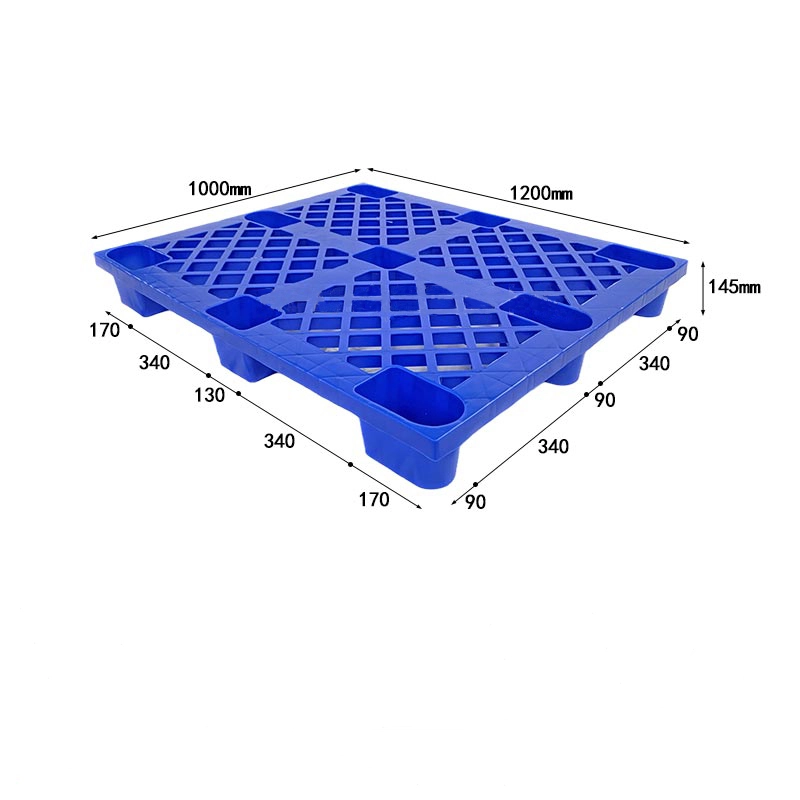
ZJ1211-145 Light-weight Nine-leg Nestable Plastic Pallet
The lightweight nine-leg nestable plastic pallet is an innovative and stylish packaging solution designed for general cargo storage and transport. It’s made of virgin HDPE or PP, featuring in space-saving due to its nine hollow feet design for nesting and cost-effectiveness.
Request More Information About Plastic Pallets
Have questions or need detailed insights on this article? Fill out the form below to contact our team for comprehensive information and support related to our plastic pallet solutions.
Contact us


+86 138 0277 8204
+86 183 4431 0917
+86 131 8916 6579

No. 15-1, Fengying Rd., Taiping Town, Conghua Dist., Guangzhou City, Guangdong Province, China.

Build the Perfect Pallet for Your Operation
Customized pallets engineered to fit your equipment, load, and workflow.
Whatsapp: +8613802778204
Scan QR Code
Guangdong Weihong Plastic Technology Co., Ltd.
Weihong
Guangdong Weihong Plastics Technology Company Ltd.