

Sample Approval Process for Nestable Plastic Pallet Orders

Efficient sample approval for nesting polymer skids reduces lead time, prevents mass-production defects, and protects supply-chain ROI by validating geometry, material behavior, and functional stacking before full-scale molding. This guide outlines a practical, stage-gated prototyping and sign-off workflow—covering dimensional validation, material qualification, hygienic and load-bearing testing, supplier contractual controls, and risk-mitigation tactics—so procurement teams and operations managers can convert approval cycles into predictable milestones while meeting regulatory and automation requirements. Citations include industry references from Wikipedia, ISO, FDA, and WHO.
- Pre‑Production Verification for Space‑Saving Polymer Skids
- Define approval objectives and measurable KPIs
- Material selection and food-safety validation
- Prototype geometry and mold feasibility checks
- Structured Sample Approval Workflow
- Stage gates: pre-sample, prototype, pilot, and PPAP
- Inspection protocols and measurement plans
- Functional testing: stacking, nesting, and handling trials
- Common Failure Modes, Root Causes and Mitigations
- Dimensional drift and mold shrinkage
- Material contamination and hygiene breaches
- Stack instability and operational safety
- Supplier Controls, Contracts and Documentation
- Technical contracts and change control
- Traceability, certificates and batch records
- Performance warranty and remediation clauses
- Transitioning from Approval to Reliable Production — The Weihong Advantage
- Manufacturing scale and tooling capability
- Material science, hygiene and sector specialization
- Design‑to‑Delivery OEM/ODM and quality governance
- Why procurement teams choose Weihong
- Frequently Asked Questions
Efficient sample approval for nesting polymer skids reduces lead time, prevents mass-production defects, and protects supply-chain ROI by validating geometry, material behavior, and functional stacking before full-scale molding. This guide outlines a practical, stage-gated prototyping and sign-off workflow—covering dimensional validation, material qualification, hygienic and load-bearing testing, supplier contractual controls, and risk-mitigation tactics—so procurement teams and operations managers can convert approval cycles into predictable milestones while meeting regulatory and automation requirements. Citations include industry references from Wikipedia, ISO, FDA, and WHO.
Pre‑Production Verification for Space‑Saving Polymer Skids
Define approval objectives and measurable KPIs
Before issuing tooling or first-shot parts, buyers should document acceptance criteria: dimensional tolerances, allowable warpage, nesting compression clearance, static and dynamic load capacity, and hygiene standards for food or pharma handling. Metrics should be specific (e.g., maximum deviation ±2.0 mm on key datum surfaces; stack height tolerance ±3 mm; static load 1,500 kg without permanent deformation). These KPIs convert subjective expectations into verifiable test protocols and reduce later disputes.
Material selection and food-safety validation
Commission material data sheets (MDS) and migration test certificates when pallets will contact consumables. For hygienic applications, require documented compliance with food-contact guidance and declarations of compliance for polymers and additives. Reference authorities such as the FDA food-contact guidance and internationally recognized quality systems to align material qualifications with buyer risk tolerances.
Prototype geometry and mold feasibility checks
Use CAD-for-manufacture reviews and try-run single-cavity prototypes to verify nesting radii, draft angles, and rib patterns. Confirm that tooling proposals include venting, cooling, and gate locations that preserve critical tolerances required for automated racking or conveyor transfer. Early tooling reviews catch manufacturability issues that otherwise cause iterative mold changes and weeks of delay.
Structured Sample Approval Workflow
Stage gates: pre-sample, prototype, pilot, and PPAP
A practical approval pipeline separates stages into clear gates: pre-sample (design sign-off), prototype (functional fit), pilot run (short production batch), and Production Part Approval Process (PPAP) or equivalent for final acceptance. Each gate requires documented evidence—inspection reports, test certificates, and acceptance sign-off from stakeholders such as engineering, quality assurance, and operations.
Inspection protocols and measurement plans
Define an inspection plan that includes dimensional inspection points, surface finish acceptance, and material verification. Use coordinate measuring machines (CMM) or laser scanning for critical datum surfaces and nesting interfaces, and produce inspection reports with measured vs. nominal values. Specify sampling methods and acceptance levels (e.g., AQL for cosmetic defects) so the supplier knows when rework or remolding is needed.
Functional testing: stacking, nesting, and handling trials
Validate the stacking behavior with nested and stacked cycles under representative loads. Test deformation after repeated nesting cycles to simulate rack turnover frequency. For automation compatibility, run conveyor and AS/RS pick tests with the actual robotic grippers and forklift tines expected in service. Document any interference or slipping that arises during real-world handling.
Common Failure Modes, Root Causes and Mitigations
Dimensional drift and mold shrinkage
Polymer shrinkage and cycle cooling cause dimensional drift that affects nest clearance and stack stability. Mitigate risk by specifying target shrinkage ranges in the technical drawing, confirming expected shrink values for chosen HDPE/PP grades, and including a mold qualification run to lock cavity dimensions before mass production.
Material contamination and hygiene breaches
Contamination risks arise when recycled content or additives are poorly specified. Require certificates of origin for polymer feedstock, batch material traceability, and periodic third‑party testing where hygiene is critical. For high‑risk sectors, insist on traceable sanitation records and surface finish criteria proven to resist bacterial entrapment in accordance with recognized guidance such as WHO hygiene recommendations.
Stack instability and operational safety
Unexpected instability during stacking often comes from inconsistent rib geometry or incorrect nest depth. Simulate worst‑case loading and perform tilt/shift tests on stacked columns. Include a safety factor in load ratings to account for dynamic impacts during transport and forklift handling.
Supplier Controls, Contracts and Documentation
Technical contracts and change control
Embed detailed technical appendices in purchase orders that lock geometry, tolerances, materials, and acceptance tests. Define an engineering change control (ECC) procedure with approval requirements for any mold alterations. This prevents unilateral supplier modifications that could invalidate previously approved samples.
Traceability, certificates and batch records
Require batch-level traceability for polymer lots, tooling serials, inspection reports, and production photographs. Store these documents in a shared portal to accelerate audits and minimize time lost when a non-conformance occurs.
Performance warranty and remediation clauses
Include warranty clauses that assign liability for premature failure due to molding defects or material non‑conformance. Define remediation actions such as rework, replacement shipments, or financial penalties for unacceptable rates of defects discovered within a defined warranty period.
| Approval Approach | Typical Cycle Time | Common Rejection Causes | Relative Cost Impact | Documentation Required |
|---|---|---|---|---|
| Ad‑hoc supplier trial | 4–10 weeks | Dimensional drift, poor nesting fit | Medium‑High (rework/remold) | Loose QA photos, verbal approvals |
| Standardized stage‑gated workflow | 3–6 weeks (predictable) | Reduced: caught in prototype/pilot stages | Lower (prevents mass rework) | Formal inspection reports, material certificates, PPAP |
| Advanced digital validation (CAD+CAE + inline inspection) | 2–5 weeks | Minimal: simulated failure modes preempted | Lowest over lifecycle | Full digital records, scan data, simulation outputs |
Notes: Typical timing and impacts vary by complexity. Predictable, documented workflows reduce downstream warranty costs and logistics disruption. For background on pallet types and handling, refer to Wikipedia - Pallet and for recognized standards and certifications consult ISO.
Transitioning from Approval to Reliable Production — The Weihong Advantage
Manufacturing scale and tooling capability
We operate a 40,000+ m² intelligent manufacturing base equipped with advanced large‑scale injection and blow molding machinery, enabling high‑precision cavity control and consistent cycle repeatability. Our tooling engineering team validates mold flow and cooling profiles before prototype release to avoid dimensional drift and ensure nesting interfaces meet automation specs.
Material science, hygiene and sector specialization
Backed by over 60 years of industry heritage and a 200 million RMB investment, Weihong produces standardized, durable, and eco‑friendly HDPE/PP solutions certified for demanding supply chains. Our hygienic platforms for Food and Pharmaceutical clients include material declarations and production zone segregation aligned with international food‑safety guidance such as the FDA framework.
Design‑to‑Delivery OEM/ODM and quality governance
Our “Design to Delivery” service model integrates industrial design, rapid prototyping, trial runs, and PPAP‑grade documentation to accelerate approvals. Buyers benefit from our OEM/ODM capabilities across product lines—plastic pallet skids, stackable transit platforms, plastic pallet boxes, plastic turnover boxes, hygienic pallets, wire mesh cage systems, and HDPE pallets—streamlining single‑source responsibility during trial and mass production.
Why procurement teams choose Weihong
We provide controlled sample cycles, full traceability, and contractual change control to minimize approval disputes. Our engineering support includes CAD review, CAE-backed flow analysis, and on‑site validation to ensure nestable designs meet both warehouse ergonomics and automation constraints. For additional assurance on design reproducibility and compliance, buyers can request factory acceptance tests and documented material certificates before greenlighting mold release.
For sector guidance and design requirements on pallet performance and safety, stakeholders may consult international standards and institutional resources such as ISO standards and public overviews like Wikipedia to align internal specifications with global benchmarks.
Guangdong Weihong Plastic Technology Co., Ltd. is a premier manufacturer of high‑performance logistic packaging, established in 2013 as a state‑owned subsidiary of the Top‑500 Guangzhou Plastic Industrial Corporation Ltd. Beyond manufacturing, we provide comprehensive OEM/ODM solutions characterized by our “Design to Delivery” service model. We specialize in solving complex logistics challenges—from hygienic pallets for the Food and Pharmaceutical sectors to high‑precision units for Automated Warehousing (AS/RS) and heavy‑duty options for Automotive manufacturing. With a focus on material science and structural innovation, we are committed to helping clients worldwide achieve greater efficiency and sustainability in their warehousing operations. Contact: yangyf@gzpl.com.cn | Website: https://www.pearlriverplastics.com
For audits or sample requests, our engineering and quality teams will provide a predefined PPAP checklist, inspection plan, and timeline so buyers can budget project milestones and reduce launch risk.
To request technical drawings, sample quotes, or to schedule a factory validation run, contact our sales engineering team by email at yangyf@gzpl.com.cn.
Frequently Asked Questions
What are the critical acceptance criteria for a nesting pallet sample?
Critical acceptance criteria include key dimensional tolerances on datum surfaces, nest clearance between adjacent units, static and dynamic load ratings, allowable warpage, surface finish for hygienic sectors, and material certifications for food contact when applicable.
How long does a typical sample approval cycle take?
A predictable, stage‑gated cycle from prototype to pilot and PPAP typically takes 3–6 weeks; advanced digital validation and well‑prepared technical packages can reduce this to 2–5 weeks depending on complexity and testing requirements.
Which tests should be run on a prototype to ensure nesting performance?
Run dimensional inspections (CMM or laser scan), repeated nesting/stacking cycles under representative loads, conveyor and AS/RS handling trials, and material verification tests. Record results in inspection reports and compare against pre‑defined KPIs.
What documentation should buyers require from suppliers during approval?
Require material data sheets, certificates of origin, inspection reports with measured versus nominal values, trial run photographs, tooling identification, and a PPAP or equivalent final acceptance package. Include engineering change control clauses in the purchase contract.
How can suppliers demonstrate hygiene compliance for pallets used in food and pharma?
Suppliers should provide polymer declarations, migration testing where applicable, production zone sanitation records, cleaning procedure documentation, and adherence to international guidance such as FDA food‑contact recommendations and recognized quality systems.
OEM/ODM plastic chicken transport cage Manufacturers and Suppliers
Stackable vs Nestable Plastic Pallets: Which Is Best for You?
Supplier Audit Checklist for Nestable Plastic Pallet Manufacturers
Heavy-Duty Plastic Pallets: Load Capacity and Racking Safety

ZJ1111-140 Light-weight Nine-leg Nestable Plastic Pallet
The lightweight nine-leg nestable plastic pallet is an innovative and stylish packaging solution designed for general cargo storage and transport. It’s made of virgin HDPE or PP, featuring in space-saving due to its nine hollow feet design for nesting and cost-effectiveness.

ZJ1208-140 Light-weight Nine-leg Nestable Plastic Pallet
The lightweight nine-leg nestable plastic pallet is an innovative and stylish packaging solution designed for general cargo storage and transport. It’s made of virgin HDPE or PP, featuring in space-saving due to its nine hollow feet design for nesting and cost-effectiveness.

ZJ1210-140M Light-weight Nine-leg Nestable Plastic Pallet
The lightweight nine-leg nestable plastic pallet is an innovative and stylish packaging solution designed for general cargo storage and transport. It’s made of virgin HDPE or PP, featuring in space-saving due to its nine hollow feet design for nesting and cost-effectiveness.
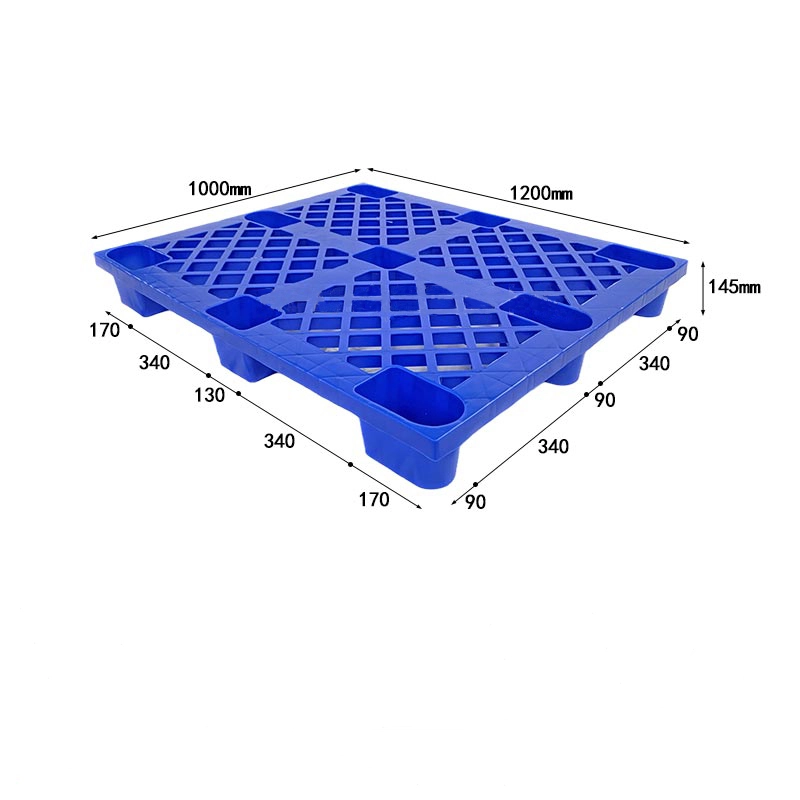
ZJ1211-145 Light-weight Nine-leg Nestable Plastic Pallet
The lightweight nine-leg nestable plastic pallet is an innovative and stylish packaging solution designed for general cargo storage and transport. It’s made of virgin HDPE or PP, featuring in space-saving due to its nine hollow feet design for nesting and cost-effectiveness.
Request More Information About Plastic Pallets
Have questions or need detailed insights on this article? Fill out the form below to contact our team for comprehensive information and support related to our plastic pallet solutions.
Contact us


+86 138 0277 8204
+86 183 4431 0917
+86 131 8916 6579

No. 15-1, Fengying Rd., Taiping Town, Conghua Dist., Guangzhou City, Guangdong Province, China.

Build the Perfect Pallet for Your Operation
Customized pallets engineered to fit your equipment, load, and workflow.
Whatsapp: +8613802778204
Scan QR Code
Guangdong Weihong Plastic Technology Co., Ltd.
Weihong
Guangdong Weihong Plastics Technology Company Ltd.