

How to Validate an Insulated Seafood Container for a Cold-Chain Route

- Quick Answer
- Key Takeaways
- What Does Cold-Chain Route Validation Mean?
- What Is the Difference Between Route Validation and Routine Monitoring?
- What Should Be Defined Before the Validation Test?
- How Should Temperature Acceptance Criteria Be Defined?
- How Should the Cold-Chain Route Be Mapped?
- How Should Challenging Cold-Chain Conditions Be Defined?
- Where Should Temperature Loggers Be Placed?
- Air Temperature vs Product Temperature: What Should Be Measured?
- What Should Be Confirmed About the Temperature Loggers?
- How Should a Representative Validation Load Be Prepared?
- How to Validate an Insulated Seafood Container for a Cold-Chain Route: 10-Step Protocol
- Should Buyers Use a Real Route Trial or a Controlled Simulation?
- How Should the Validation Results Be Evaluated?
- What Should a Cold-Chain Validation Report Include?
- When Should a Cold-Chain Route Be Revalidated?
- Seasonal Variation: Does One Test Cover the Whole Year?
- How Should Validation Results Be Used in Routine Operations?
- How Does Container Cleaning Affect Route Validation?
- Should Supplier Test Data Replace the Buyer's Route Validation?
- Common Cold-Chain Route Validation Mistakes
- Frequently Asked Questions
- Conclusion
- Define Your Cold-Chain Validation Requirements
COLD-CHAIN ROUTE VALIDATION
Quick Answer
To validate an insulated seafood container for a cold-chain route, first define the product temperature acceptance criteria and map the complete route. Then test the intended container with a representative seafood load, packing pattern, coolant method, starting temperatures, handling process, and realistic ambient conditions.
Use suitable temperature loggers at positions selected to detect meaningful temperature differences, record route events and delays, and compare the resulting time-temperature profiles with predefined acceptance criteria.
A successful test validates only the configuration and conditions that were actually evaluated. Changes to the container, product, coolant, packing pattern, route, season, vehicle, handling process, or expected delay conditions may require additional assessment.
VALIDATE THE SYSTEM
- Define product and route
- Set acceptance criteria first
- Use representative load conditions
- Plan meaningful logger positions
- Record route events and delays
- Evaluate against predefined criteria
- Define the operating envelope
Route validation should evaluate the complete shipping system, not the insulated container in isolation.
For broader guidance on container selection, procurement, handling, and cold-chain planning, see the reusable seafood transport container selection guide.
Key Takeaways
Validate the complete shipping configuration, not an empty container alone.
Define acceptance criteria before reviewing the test results.
Use a representative seafood load, packing pattern, coolant method, and starting condition.
Include reasonably foreseeable challenging route conditions.
Select logger positions according to load geometry and thermal risk rather than using one arbitrary monitoring point.
Record handling events, delays, lid openings, and route conditions alongside temperature data.
Make the pass, adjustment, or repeat decision against predefined criteria.
Define the operating envelope and reassess the route after significant process changes.
VALIDATION DEFINITION
What Does Cold-Chain Route Validation Mean?
Cold-chain route validation is a structured process used to determine whether a defined shipping configuration can meet predefined temperature and operating requirements under specified route conditions.
Some organizations may use terms such as route qualification, thermal qualification, or shipping-lane qualification. Terminology varies, so the protocol should clearly define the test objective, configuration, monitoring method, and acceptance criteria.
The configuration may include:
- Exact container model
- Container condition
- Seafood product or representative test load
- Product quantity
- Packing geometry
- Inner packaging
- Coolant type
- Coolant quantity
- Coolant placement
- Starting product temperature
- Starting coolant condition
- Lid configuration
- Vehicle or transport mode
- Route duration
- Ambient exposure
- Loading and unloading process
- Transfer stages
- Expected delays
The objective is not to prove that a container will perform identically everywhere.
Can this defined shipping configuration meet the buyer's predefined acceptance criteria under the conditions represented by the validation?
Validation Is Configuration-Specific
A result from one configuration should not automatically be applied to another.
A change in any of the following may affect thermal behavior:
- Container size
- Product mass
- Seafood type
- Starting temperature
- Coolant amount
- Coolant location
- Headspace
- Inner packaging
- Route duration
- Vehicle
- Ambient conditions
The validation report should therefore describe the tested configuration clearly enough that the buyer can understand what the result does—and does not—support.
VALIDATION VS MONITORING
What Is the Difference Between Route Validation and Routine Monitoring?
Validation and routine shipment monitoring answer different questions.
| Factor | Route Validation | Routine Monitoring |
|---|---|---|
| Main purpose | Demonstrate whether a defined configuration can meet acceptance criteria | Monitor actual operating shipments |
| Timing | Before implementation or after significant change | During routine operations |
| Test design | Planned protocol | Established operating procedure |
| Challenging conditions | May intentionally include representative challenging conditions | Reflects conditions of the actual shipment |
| Sensor plan | Selected to evaluate the configuration | Selected according to the monitoring program |
| Result | Pass, adjust, repeat, or limit operating envelope | Shipment record, excursion investigation, or release decision |
| Output | Validation report | Operational monitoring record |
Validation does not replace routine monitoring.
Routine monitoring also does not automatically validate an inadequately defined shipping configuration.
The two activities can support each other: validation establishes the operating basis, while routine data can show whether actual shipments continue to operate within that basis.
TEST DEFINITION
What Should Be Defined Before the Validation Test?
Do not start a validation by placing a logger inside a container and sending it on a route. First define exactly what is being tested.
Define the Seafood Product
Record information relevant to thermal behavior and acceptance, such as:
- Seafood type
- Fresh, chilled, or frozen condition
- Starting product temperature
- Product dimensions
- Product quantity
- Product mass
- Packaging format
- Direct or indirect contact with the container
- Inner liner or secondary packaging
- Product arrangement
The test protocol should use the actual product where practical or a justified representative load.
Define the Container Configuration
Record:
- Exact container model
- Internal dimensions where confirmed
- Lid configuration
- Drain configuration where applicable
- Inserts or dividers where applicable
- Container condition
- Preconditioning method where used
Do not substitute general manufacturer information for model-specific values that have not been confirmed.
Define the Coolant Configuration
Record:
- Coolant type
- Starting coolant condition
- Quantity
- Location
- Distribution
- Packaging
- Replenishment, if part of the actual route
Avoid using a generic coolant percentage that has not been validated for the specific configuration. The same quantity of coolant can perform differently when its placement, product load, headspace, starting temperature, or route conditions change.
Define the Route
Map the route from product preparation through receiving.
Preconditioning → Packing → Staging → Loading Dock → Vehicle Loading → Main Transport → Transfer or Cross-Dock → Final Delivery → Receiving
Important route variables may include:
- Planned duration
- Maximum realistic duration
- Refrigerated or non-refrigerated stage
- Ambient exposure
- Loading-dock time
- Vehicle temperature condition
- Transfer duration
- Number of stops
- Lid openings
- Traffic delay
- Customs or inspection delay where applicable
- Receiving delay
- Final unloading conditions
A container can perform differently on two routes of equal total duration if the handling and ambient-exposure patterns are different.
ACCEPTANCE CRITERIA
How Should Temperature Acceptance Criteria Be Defined?
Acceptance criteria should be defined before the test is run.
Do not collect data first and then decide what result should count as acceptable.
| Acceptance Input | Defined Requirement |
|---|---|
| Starting product temperature | |
| Target product temperature range | |
| Maximum permitted temperature | |
| Minimum permitted temperature where relevant | |
| Maximum permitted excursion duration | |
| Planned route duration | |
| Maximum validation duration | |
| Receiving temperature requirement | |
| Product-condition requirement | |
| Data completeness requirement | |
| Logger accuracy requirement | |
| Corrective-action rule | |
| Pass/fail decision rule |
The correct criteria depend on the actual seafood product, food-safety program, customer requirements, quality requirements, route, and applicable market rules.
Food Safety and Product Quality Are Not Always the Same Criterion
A validation may need to consider more than one objective, such as:
- Food-safety temperature requirement
- Customer receiving specification
- Product-quality target
- Frozen-state requirement
- Maximum excursion
- Container integrity
- Leakage
- Product damage
The validation report should distinguish these requirements instead of combining them into one vague statement such as “the seafood remained cold.”
Do Not Change the Pass Criteria After Seeing the Results
A test becomes difficult to interpret when the acceptance rule changes after the data are reviewed.
- Run the test.
- Observe an excursion.
- Increase the acceptable temperature limit.
- Declare the test successful.
If the original acceptance criterion was inappropriate, document why it was revised and repeat or formally reassess the validation under the revised protocol.
ROUTE MAPPING
How Should the Cold-Chain Route Be Mapped?
Route mapping identifies where the shipping system is exposed to thermal and handling risk.
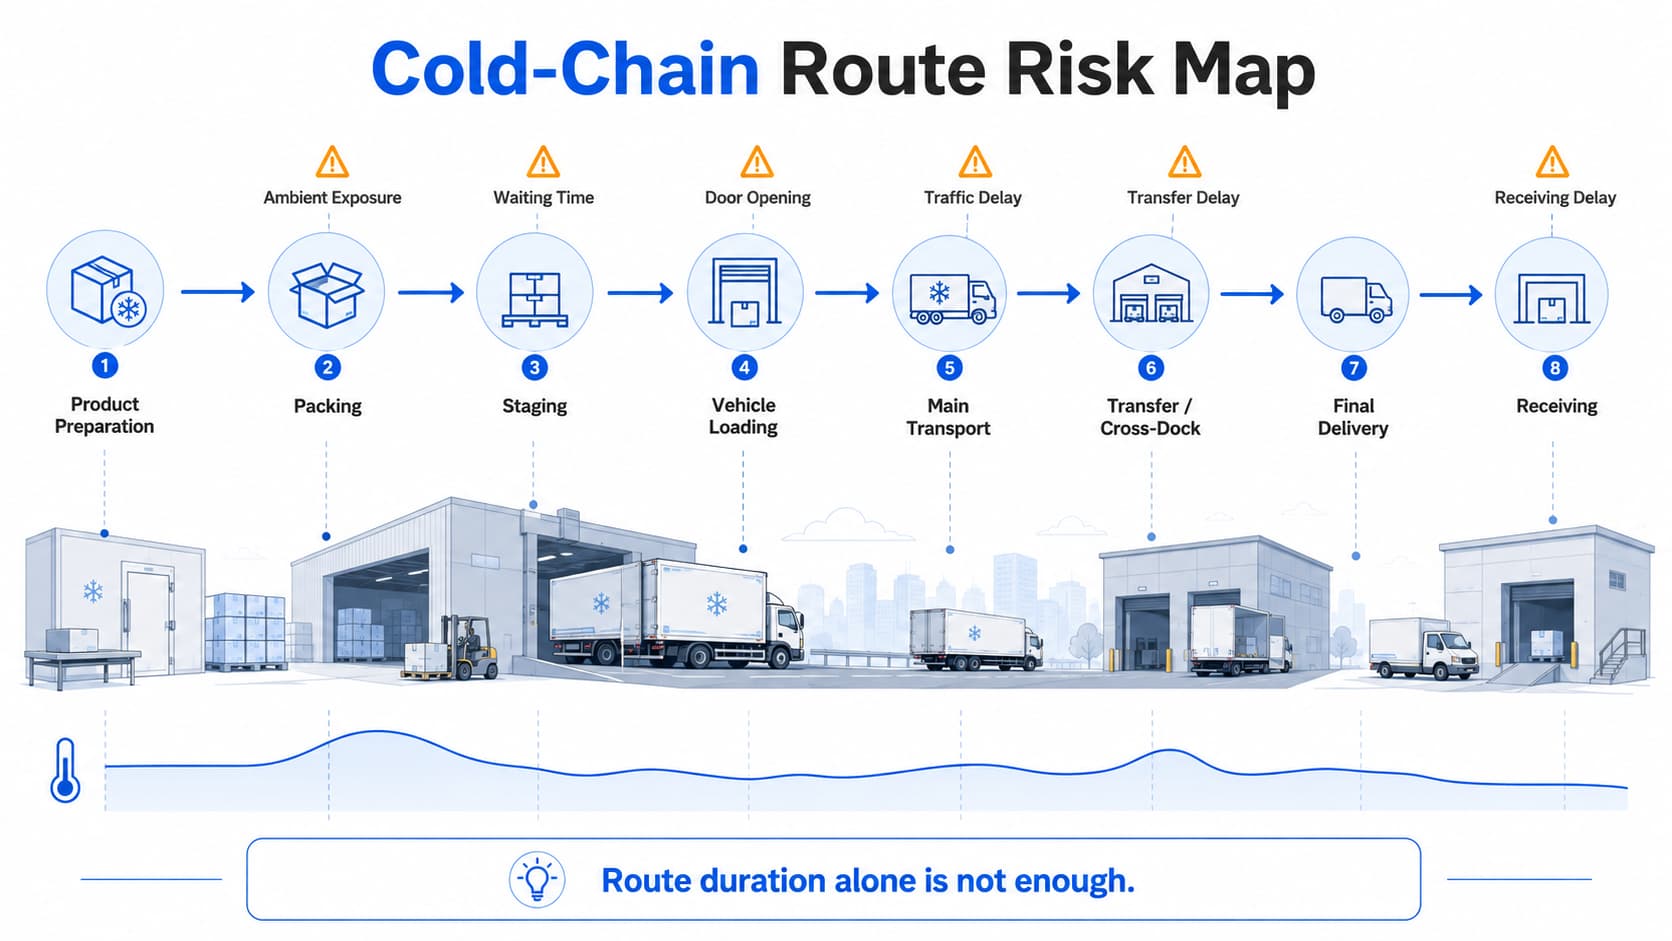
Stage 1: Product Preparation
- Product starting condition
- Product temperature
- Packing start time
- Coolant preparation
- Container condition
Stage 2: Packing
- Product quantity
- Packing pattern
- Coolant quantity
- Coolant position
- Headspace
- Lid closure time
Stage 3: Staging
- Waiting time
- Ambient exposure
- Location
- Refrigerated or non-refrigerated holding
Stage 4: Vehicle Loading
- Loading duration
- Vehicle condition
- Door opening
- Container position where relevant
Stage 5: Main Transport
- Departure
- Planned route
- Actual route
- Vehicle conditions
- Stops
- Delays
- Refrigeration interruptions where relevant
Stage 6: Transfer or Cross-Dock
- Transfer time
- Ambient conditions
- Door opening
- Handling
- Re-staging
Stage 7: Final Delivery
- Arrival time
- Waiting time
- Unloading duration
- Ambient exposure
Stage 8: Receiving
- Receiving time
- Logger stop time
- Product condition
- Product temperature where required
- Coolant condition
- Container condition
- Leakage or damage
Example Route-Mapping Table
| Route Stage | Planned Duration | Maximum Realistic Duration | Temperature Controlled? | Ambient Exposure | Lid Opening | Delay Risk |
|---|---|---|---|---|---|---|
| Packing | ||||||
| Staging | ||||||
| Loading | ||||||
| Main transport | ||||||
| Transfer | ||||||
| Final delivery | ||||||
| Receiving |
The completed map can later be compared with the logger record to explain when and why temperature changes occurred.
CHALLENGING CONDITIONS
How Should Challenging Cold-Chain Conditions Be Defined?
A useful validation should include conditions that are challenging enough to represent realistic operating risk.
In some validation programs these may be described as worst-case conditions. In this guide, the term challenging conditions means reasonably foreseeable operating conditions that place greater thermal or operational stress on the defined cold-chain process.
It does not mean combining every imaginable extreme into an unrealistic test.
Potential variables include:
- Hottest expected operating season
- Longest realistic route
- Maximum normal loading delay
- Expected traffic delay
- Long receiving delay
- Multiple delivery stops
- Higher acceptable starting product temperature
- Longer staging period
- Vehicle-refrigeration interruption where relevant to the risk scenario
- Different normal load quantities
- Realistic variation in coolant preparation
- Realistic variation in coolant placement
Is the Heaviest Load Always the Most Challenging Thermal Case?
Not necessarily.
Maximum product mass may create one challenging condition, but another configuration may be more difficult because of:
- Larger headspace
- Lower thermal mass
- Different coolant-to-product distribution
- Air gaps
- Different product geometry
- Less effective coolant contact
- Greater warm-air exposure during handling
The validation team should identify the relevant challenging configuration through route analysis, product knowledge, preliminary testing, or risk assessment.
Do not automatically assume: maximum payload = most challenging thermal case.
Should More Than One Load Configuration Be Tested?
Potentially.
If the same container is routinely used with very different:
- Fill levels
- Seafood types
- Packing arrangements
- Coolant quantities
- Shipment durations
Then a single configuration may not represent the full operating range. The validation plan should define the operating envelope the test is intended to support.
LOGGER PLACEMENT
Where Should Temperature Loggers Be Placed?
Logger placement should be based on the test objective and expected temperature variation. One arbitrary logger position may not adequately characterize a complex shipment.
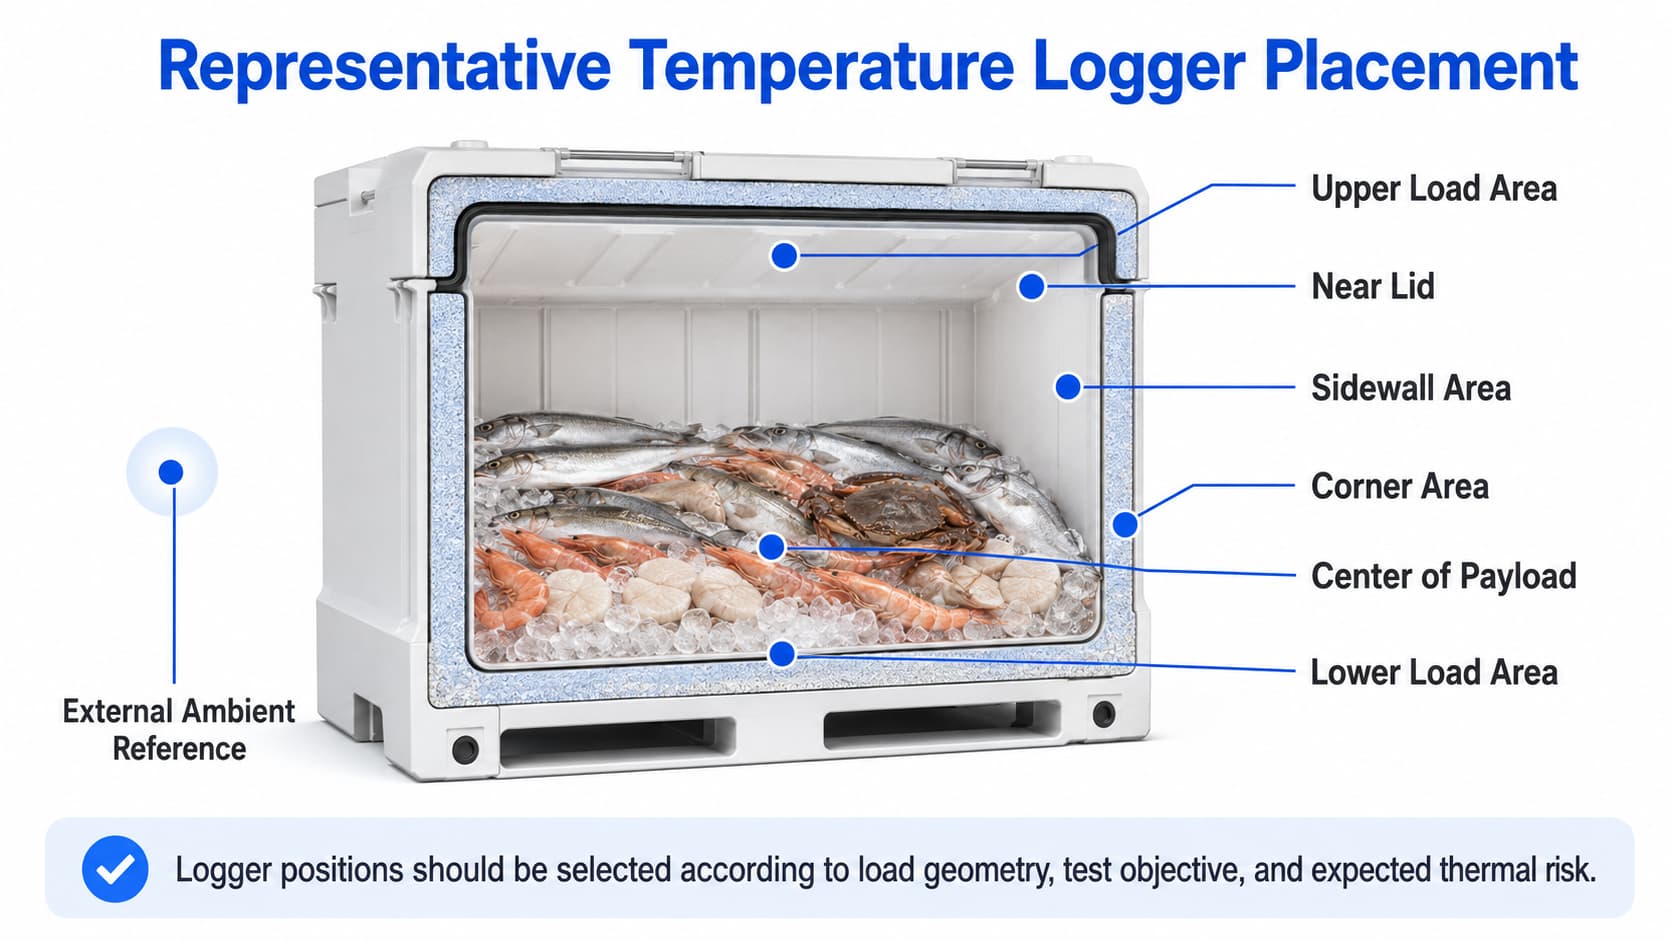
Possible monitoring positions may include:
- Near an area expected to warm quickly
- Near the upper load
- Near the lid area
- Near a sidewall
- Near a corner
- Near the center of the representative payload
- Near the lower load
- Within different containers when multiple units are tested
- Outside the container as an ambient reference
These are possible test positions, not a universal placement rule.
Do Not Use a Fixed Logger Count Without a Reason
There is no universal rule that every insulated seafood-container test must use:
- 3 loggers
- 5 loggers
- 10 loggers
The logger quantity should be justified by factors such as:
- Load size
- Container geometry
- Expected thermal gradients
- Test objective
- Preliminary mapping
- Route complexity
- Risk level
- Required confidence
A small or simple configuration may require fewer measurement points than a complex load.
A high-risk or poorly characterized configuration may justify more.
TEMPERATURE MEASUREMENT
Air Temperature vs Product Temperature: What Should Be Measured?
The validation protocol should define the measurement objective.
Air Temperature
Air temperature can help show:
- The thermal environment inside the container
- Exposure near the lid
- Warm-air entry
- Changes during openings or transfers
However, air temperature may change faster than the seafood itself.
Product or Product-Simulating Temperature
A probe placed to represent product temperature may better answer a question related to:
- Actual seafood temperature
- Product thermal response
- Product acceptance criteria
However, sensor placement and contact method affect what the measurement represents.
Ambient Temperature
An external logger may help interpret:
- High ambient exposure
- Dock conditions
- Seasonal heat
- Vehicle or transfer environment
Define the Measurement Before the Test
Do not mix air temperature, product temperature, surface temperature, and ambient temperature and treat them as interchangeable.
The validation report should identify what each logger was intended to measure.
LOGGER CONTROL
What Should Be Confirmed About the Temperature Loggers?
Before the trial, document:
- Logger ID
- Sensor type
- Measurement range
- Accuracy requirement
- Accuracy-check or calibration status
- Logging interval
- Start time
- Time synchronization
- Sensor location
- Data-retrieval method
A logger with unexplained time drift, missing data, an unsuitable range, or uncertain accuracy can weaken the validation result.
Logging Interval
Do not choose a universal interval simply because it is common.
The interval should be short enough to capture meaningful route events while providing a complete and manageable data record.
A route involving:
- Short loading events
- Frequent stops
- Rapid environmental changes
May need a different interval from a long, stable transport process.
REPRESENTATIVE LOAD
How Should a Representative Validation Load Be Prepared?
A validation load should reproduce the actual operating configuration as closely as practical.
Use the Actual Seafood Where Practical
If the test uses real product, document:
- Product
- Quantity
- Starting temperature
- Dimensions
- Packaging
- Packing pattern
- Coolant placement
If a Simulated Load Is Used
A simulated load should reproduce the relevant characteristics of the actual shipment as closely as practical.
- Weight
- Volume
- Thermal mass
- Packing geometry
- Headspace
- Coolant arrangement
- Starting temperature
Do not assume that any convenient substitute automatically represents seafood correctly.
The simulation should be justified according to the test objective.
Precondition the Test Components
Where relevant, define the starting condition of:
- Product
- Simulated load
- Container
- Coolant
- Vehicle
- Staging environment
If one test begins with a substantially colder product or coolant than the real operation, the result may overstate the practical thermal margin.
Reproduce the Real Packing Pattern
Document:
- Number of product units
- Total mass
- Arrangement
- Inner packaging
- Coolant location
- Coolant quantity
- Headspace
- Lid closure
- Container orientation
For guidance on matching container capacity and packing configuration to the route, see how to choose seafood transport container capacity.
10-STEP VALIDATION PROTOCOL
How to Validate an Insulated Seafood Container for a Cold-Chain Route: 10-Step Protocol
A structured protocol helps prevent important variables from changing unnoticed during testing.
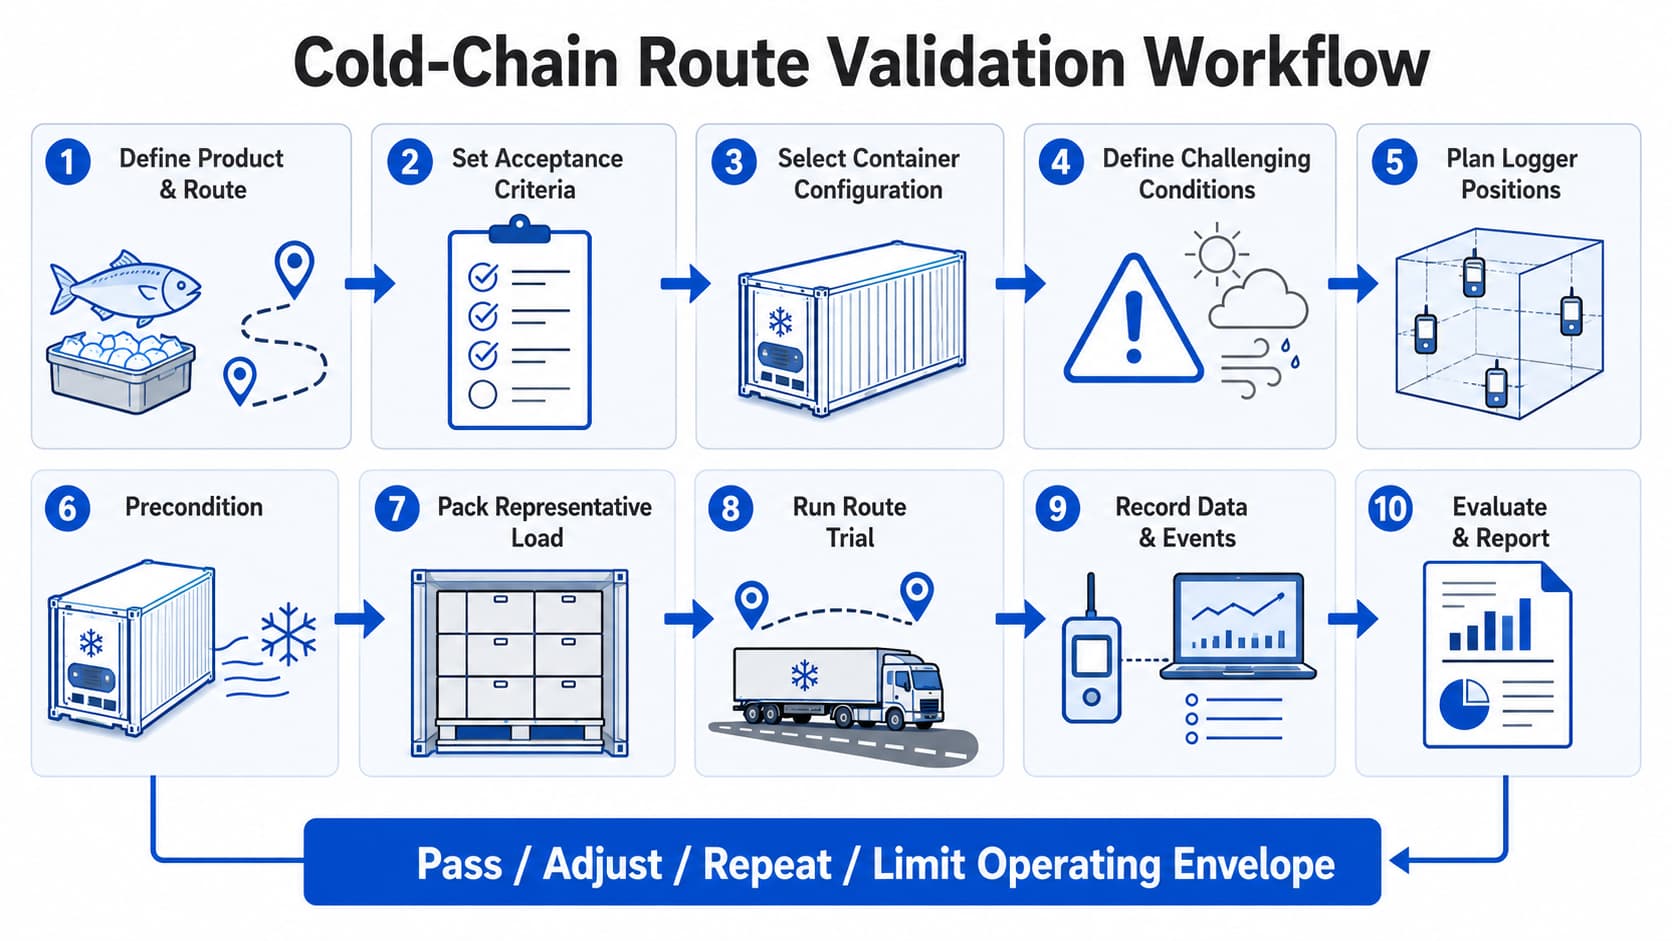
Step 1: Define the Product and Route
Document:
- Seafood
- Product condition
- Quantity
- Origin
- Destination
- Route stages
- Planned duration
- Handling steps
Step 2: Set Predefined Acceptance Criteria
Before collecting data, define:
- Temperature criteria
- Excursion criteria
- Duration criteria
- Product-condition criteria
- Data-quality criteria
- Pass/fail rule
Step 3: Select the Exact Container Configuration
Record:
- Container model
- Container condition
- Lid
- Drain configuration where applicable
- Inserts or liners where applicable
Do not switch container models during the validation without documenting the change.
Step 4: Define Representative and Challenging Conditions
Identify:
- Normal route
- Longer realistic route
- Relevant seasonal condition
- Delay scenario
- Load condition
- Coolant variation
- Transfer exposure
The selected test scenario should be justified.
Step 5: Prepare the Logger and Sensor Plan
Document:
- Logger IDs
- Measurement objective
- Sensor positions
- Ambient reference where used
- Logging interval
- Accuracy or calibration status
- Time synchronization
Step 6: Precondition Product, Coolant, Container, and Equipment
Prepare the test so the starting conditions represent the intended operating process. Record any deviations.
Step 7: Pack the Representative Load
Follow the defined:
- Product quantity
- Packing arrangement
- Coolant quantity
- Coolant placement
- Inner packaging
- Headspace
- Closure method
Record the packing completion time.
Step 8: Run the Route Trial or Controlled Simulation
Operate the trial according to the protocol.
Record actual:
- Departure
- Arrival
- Route changes
- Stops
- Transfers
- Delays
- Lid openings
- Environmental events
- Vehicle interruptions
Do not change coolant quantity, packing pattern, sensor position, or acceptance criteria during the test without documenting the change.
Step 9: Record Temperature, Route Events, and Receiving Condition
At completion, collect:
- Logger data
- Ambient data where used
- Receiving product temperature where required
- Product condition
- Coolant condition
- Leakage
- Container damage
- Packing movement
- Actual duration
- Deviations
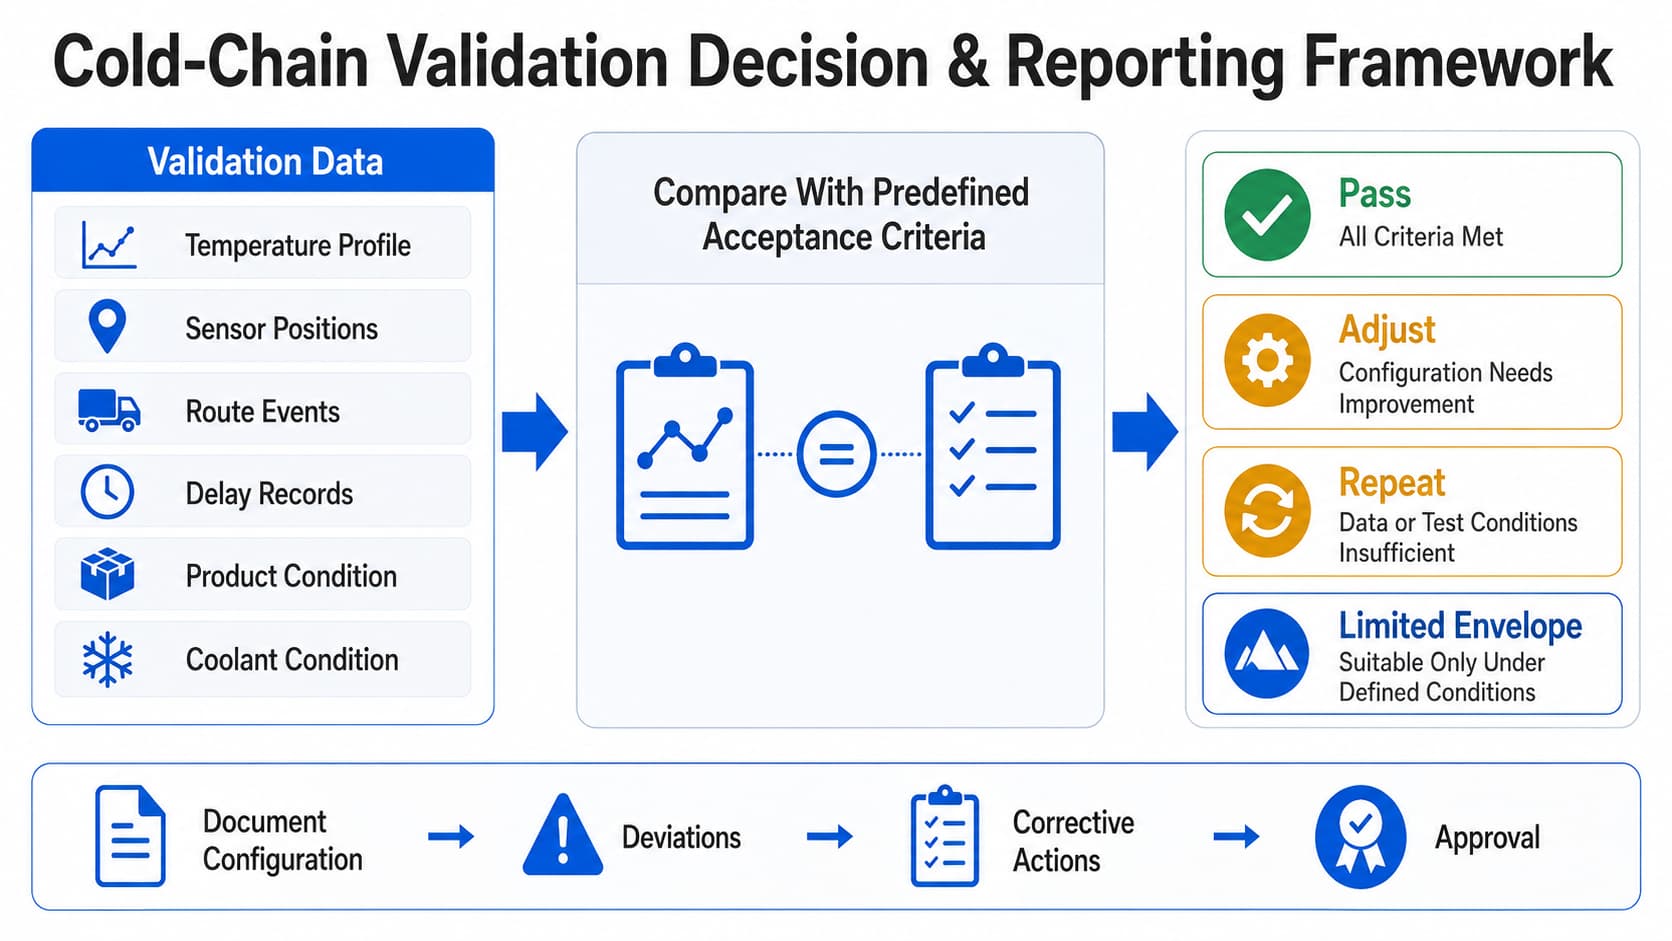
Step 10: Compare the Results With the Acceptance Criteria
The conclusion should be based on the criteria defined before the test.
Pass
The tested configuration met all defined acceptance criteria.
Adjust
The result identified a configuration or operating condition that needs improvement.
Repeat
The test was incomplete, data quality was insufficient, conditions were not representative, or the configuration changed.
Limit the Operating Envelope
The configuration may be suitable only under defined conditions such as a shorter duration, specific load arrangement, or seasonal range.
TEST METHOD
Should Buyers Use a Real Route Trial or a Controlled Simulation?
Both approaches can be useful, but they answer different questions.
| Factor | Real Route Trial | Controlled Simulation |
|---|---|---|
| Actual handling | Captured directly | Must be reproduced |
| Traffic and route delays | Real | Simulated |
| Receiving process | Real | May be simplified |
| Environmental control | Limited | Greater control |
| Repeatability | Lower | Higher |
| Specific temperature profile | Weather dependent | Can be intentionally reproduced |
| Operational realism | High | Depends on test design |
Advantages of a Real Route Trial
A real route can reveal issues such as:
- Long loading delays
- Vehicle-door openings
- Unexpected waiting
- Poor transfer practices
- Receiving delays
- Handling variation
These may be difficult to reproduce perfectly in a controlled facility.
Advantages of Controlled Simulation
A controlled test may allow the validation team to:
- Repeat the same environmental profile
- Compare two packing configurations
- Test a defined high-temperature condition
- Change one variable at a time
- Investigate a previous failure
They May Be Used Together
A controlled simulation can characterize thermal behavior.
A real route can show whether the operational process introduces additional risk.
Depending on the buyer's risk assessment, the two methods may complement each other.
RESULT EVALUATION
How Should the Validation Results Be Evaluated?
Do not evaluate only the final temperature.
The full data record may reveal problems that the receiving reading misses.
Review:
- Starting temperature
- Highest relevant temperature
- Lowest relevant temperature where applicable
- Time-temperature profile
- Excursion duration
- Differences between sensor positions
- Time of significant temperature change
- Route-event timing
- Lid-opening events
- Delay periods
- Ambient conditions
- Coolant condition
- Product condition
- Leakage
- Packaging movement
- Container damage
Compare Sensor Positions
If one sensor is consistently warmer than the others, ask:
- Was it near the lid?
- Was coolant distribution different?
- Was there more headspace?
- Was it closer to a sidewall?
- Was it affected by an opening?
- Was the logger position correct?
- Did the load shift?
Temperature variation can identify weaknesses that an average value hides.
Compare Data With Route Events
Temperature rise began during a 45-minute receiving delay.
This is more operationally useful than simply reporting a maximum temperature without context.
Route-event correlation helps determine whether corrective action should involve:
- Container configuration
- Coolant
- Loading process
- Vehicle
- Route timing
- Receiving process
Use Predefined Decision Categories
Pass
All predefined requirements were met.
Adjustment Required
The result identifies a configuration or process condition that needs improvement.
Repeat Test
Repeat when data, starting conditions, route conditions, packing, or test configuration are not sufficient to support the conclusion.
Possible adjustment findings may include:
- Insufficient delay margin
- A consistently warmer location within the load
- Coolant distribution needing revision
- Packing arrangement needing adjustment
- An operational delay requiring additional control
Repeat may be appropriate when:
- Logger data are incomplete
- A logger failed
- Starting conditions were outside the protocol
- The actual route differed materially from the test design
- The load was packed incorrectly
- A configuration was changed during the trial
Fail
A fail conclusion is appropriate when one or more predefined acceptance criteria were not met and the result cannot be justified within the intended operating envelope.
Do not remove an unfavorable logger result simply to make the validation pass.
VALIDATION REPORT
What Should a Cold-Chain Validation Report Include?
The validation report should make the test reproducible and understandable.
Example Validation Report
| Validation Report Field | Record |
|---|---|
| Test ID | |
| Test date | |
| Test objective | |
| Container model | |
| Container condition | |
| Seafood product or simulated load | |
| Product quantity | |
| Product mass | |
| Starting product temperature | |
| Coolant type | |
| Coolant quantity | |
| Coolant starting condition | |
| Coolant placement | |
| Packing pattern | |
| Inner packaging | |
| Route | |
| Ambient conditions | |
| Vehicle or transport mode | |
| Sensor/logger ID | |
| Sensor purpose | |
| Sensor location | |
| Accuracy/calibration status | |
| Logging interval | |
| Planned route duration | |
| Actual route duration | |
| Delay events | |
| Lid-opening events | |
| Transfer events | |
| Temperature results | |
| Product condition at receipt | |
| Coolant condition at receipt | |
| Leakage or damage | |
| Acceptance criteria | |
| Deviations | |
| Corrective actions | |
| Final result | Pass / Adjust / Repeat / Limited Envelope |
| Reviewer | |
| Approval |
Add a Configuration Statement
The report should clearly state what was validated.
The result applies to the container, load, coolant, packing configuration, route, and operating conditions described in this report.
Avoid vague conclusions such as “Container validated.” That statement does not explain which configuration or route the validation supports.
Define the Operating Envelope
A validation can establish a defined operating envelope.
The envelope might include:
- Approved container model
- Product or product category
- Load range
- Coolant configuration
- Starting-temperature limit
- Route-duration limit
- Ambient condition
- Vehicle condition
- Seasonal condition
- Handling limits
Do not expand the envelope beyond the evidence generated by the validation.
CHANGE CONTROL
When Should a Cold-Chain Route Be Revalidated?
A validation should be reviewed when important variables change.
Possible change-control triggers include:
- New container model
- Container design change
- Seafood product change
- Product-packaging change
- Major load-quantity change
- New packing pattern
- Coolant type change
- Coolant quantity change
- Coolant placement change
- New route
- Longer route duration
- New transfer stage
- New vehicle type
- Different seasonal conditions
- Repeated temperature excursions
- Major facility change
- Major loading or receiving-process change
Not every small operational change automatically requires a complete new validation.
The buyer should assess whether the change moves the operation outside the validated envelope or introduces a new thermal risk.
SEASONAL CONDITIONS
Seasonal Variation: Does One Test Cover the Whole Year?
Not automatically.
A route tested during mild weather may not represent:
- Hot-season loading
- High solar exposure
- Cold-season freezing risk where relevant
- Seasonal traffic
- Longer holiday delays
- Different vehicle conditions
The validation plan should determine which seasonal conditions are relevant to the route.
Possible approaches include:
- Separate seasonal trials
- Controlled simulation of challenging ambient conditions
- Additional monitoring during a new season
- Defined operating limits
The correct strategy depends on the product, route, climate, and risk.
ROUTINE OPERATIONS
How Should Validation Results Be Used in Routine Operations?
Once the configuration has been validated, the resulting information can support operating procedures.
These may include:
- Approved packing pattern
- Approved coolant arrangement
- Starting-temperature requirements
- Maximum route duration
- Loading controls
- Logger placement
- Receiving checks
- Excursion investigation
- Revalidation triggers
Routine operations should remain within the validated operating envelope.
If repeated shipment data show that the route regularly operates close to the limit, the buyer should consider whether additional margin or a revised configuration is needed.
CONTAINER CONDITION
How Does Container Cleaning Affect Route Validation?
Cleaning and thermal validation are separate activities, but a reusable container's condition can affect whether a test configuration remains representative.
Before testing, check whether the container:
- Is clean
- Is dry where required
- Has all required components
- Has no disqualifying damage
- Is in the intended service condition
A damaged or improperly prepared container may produce results that do not represent normal operation.
For a detailed sanitation workflow, see how to clean and sanitize reusable seafood transport containers.
SUPPLIER DATA
Should Supplier Test Data Replace the Buyer's Route Validation?
Not automatically.
Supplier data may help the buyer understand:
- Test methods
- Configuration
- General thermal behavior
- Available technical documentation
However, supplier testing may use different:
- Loads
- Coolant
- Ambient conditions
- Starting temperatures
- Routes
- Sensor positions
- Durations
- Packing patterns
The buyer should compare the supplier's test configuration with the actual intended route.
Supplier data are most useful when the tested conditions are relevant to the buyer's operating configuration.
They should not automatically be treated as proof that every real-world route will meet the buyer's requirements.
COMMON ERRORS
Common Cold-Chain Route Validation Mistakes
1. Testing an Empty Container
An empty container does not represent the thermal behavior of a loaded seafood shipment.
2. Setting Acceptance Criteria After Seeing the Data
Define the decision rule before the trial.
3. Using Only One Arbitrary Temperature Logger
One measurement point may miss temperature variation within the load.
4. Recording Temperature Without Route Events
Without time-stamped handling information, it can be difficult to explain why a temperature change occurred.
5. Testing Only Ideal Conditions
A validation with no realistic thermal or operational challenge may not support the intended route.
6. Ignoring Loading and Receiving Delays
The warmest exposure may occur while the container is waiting rather than while the vehicle is moving.
7. Changing the Packing Pattern After Validation
A different product distribution, headspace, or coolant position can change thermal behavior.
8. Treating Air and Product Temperature as the Same Measurement
They answer different questions and may respond at different rates.
9. Applying One Result to Every Season, Route, or Customer
Validation should have a defined operating envelope.
10. Treating Supplier Laboratory Data as Proof of the Buyer's Actual Route
Supplier data can support evaluation, but actual route conditions may be different.
11. Ignoring Logger Accuracy or Time Synchronization
Unreliable or unsynchronized data can make route-event analysis difficult.
12. Looking Only at the Final Temperature
A temporary excursion during transit can be missed if only the receiving measurement is reviewed.
FREQUENTLY ASKED QUESTIONS
Frequently Asked Questions
How do you validate an insulated seafood container for a cold-chain route?
Define the seafood product, container, coolant, packing configuration, route, starting conditions, temperature-monitoring plan, and acceptance criteria before the test. Run a representative route trial or controlled simulation, record time-temperature data and route events, compare the results with the predefined criteria, and document whether the tested configuration passes, requires adjustment, or should be tested again.
What should be included in a cold-chain route validation?
A validation should define the container model, seafood or representative load, product quantity, starting temperature, coolant method, packing pattern, route, realistic challenging conditions, temperature logger plan, acceptance criteria, handling events, actual duration, temperature results, deviations, product condition, and final validation decision.
Where should temperature loggers be placed in an insulated seafood container?
Logger positions should be selected according to the load geometry, test objective, expected thermal gradients, and preliminary risk assessment. Possible positions include the upper load, near the lid, sidewall or corner areas, the center of the payload, lower areas, and an external ambient reference. There is no universal sensor position or fixed logger count that fits every configuration.
Should route validation measure air temperature or product temperature?
It depends on the acceptance criterion and test objective. Air temperature describes the environment around the load, while product or product-simulating measurements may better represent the thermal condition of the seafood. The validation protocol should define what each sensor is intended to measure and should not treat air, product, surface, and ambient temperatures as interchangeable.
How should challenging cold-chain conditions be defined?
Use reasonably foreseeable conditions that challenge the defined route, such as a longer realistic duration, seasonal heat, loading or receiving delays, multiple stops, or representative variation in load and coolant configuration. Challenging conditions should be justified by route risk rather than created by combining unrelated extreme conditions into an unrealistic test.
How many validation trials are required?
There is no universal number that applies to every cold-chain route. The number of trials should reflect route variability, seasonal conditions, load configurations, product risk, test objectives, data quality, applicable quality requirements, and the level of confidence needed to support the intended operating envelope.
Can a simulated payload be used for seafood container validation?
A simulated load may be useful when it can reasonably reproduce relevant characteristics such as mass, volume, thermal behavior, geometry, headspace, starting temperature, and coolant arrangement. The simulation should be justified for the intended test objective and should not be assumed to represent seafood accurately without evaluation.
When should a cold-chain route be revalidated?
Revalidation or additional assessment may be appropriate after significant changes to the container, seafood product, load configuration, coolant method, route, vehicle, transport duration, transfer process, seasonal conditions, or handling procedure, or when repeated excursions suggest that the current operating envelope may no longer be adequate.
FINAL CHECK
Conclusion
Validating an insulated seafood transport container means validating a defined shipping system, not simply measuring the temperature inside an empty box.
A strong route-validation process should:
- Define the product and route.
- Establish acceptance criteria before testing.
- Reproduce the intended container, load, packing, and coolant configuration.
- Include realistic challenging operating conditions.
- Use justified logger positions.
- Record route events alongside temperature data.
- Evaluate the complete time-temperature profile.
- Document deviations.
- Make a predefined pass, adjustment, or repeat decision.
- Define the operating envelope.
- Reassess the validation when significant conditions change.
The most useful validation report does not say only:
“The container passed.”
It explains:
Which container, load, coolant, packing method, route, environmental conditions, monitoring plan, and acceptance criteria were evaluated—and under what conditions the result applies.
NEXT STEP
Define Your Cold-Chain Validation Requirements
Share your seafood product, starting temperature, target temperature requirements, route duration, ambient conditions, coolant method, packing configuration, container size, vehicle conditions, handling stages, expected delays, shipment quantity, destination market, and technical-documentation needs.
Review the insulated seafood transport container range listed on the Weihong website, or contact Weihong to discuss the container information and technical details needed for your route-evaluation process.
Discuss Your Validation Requirements
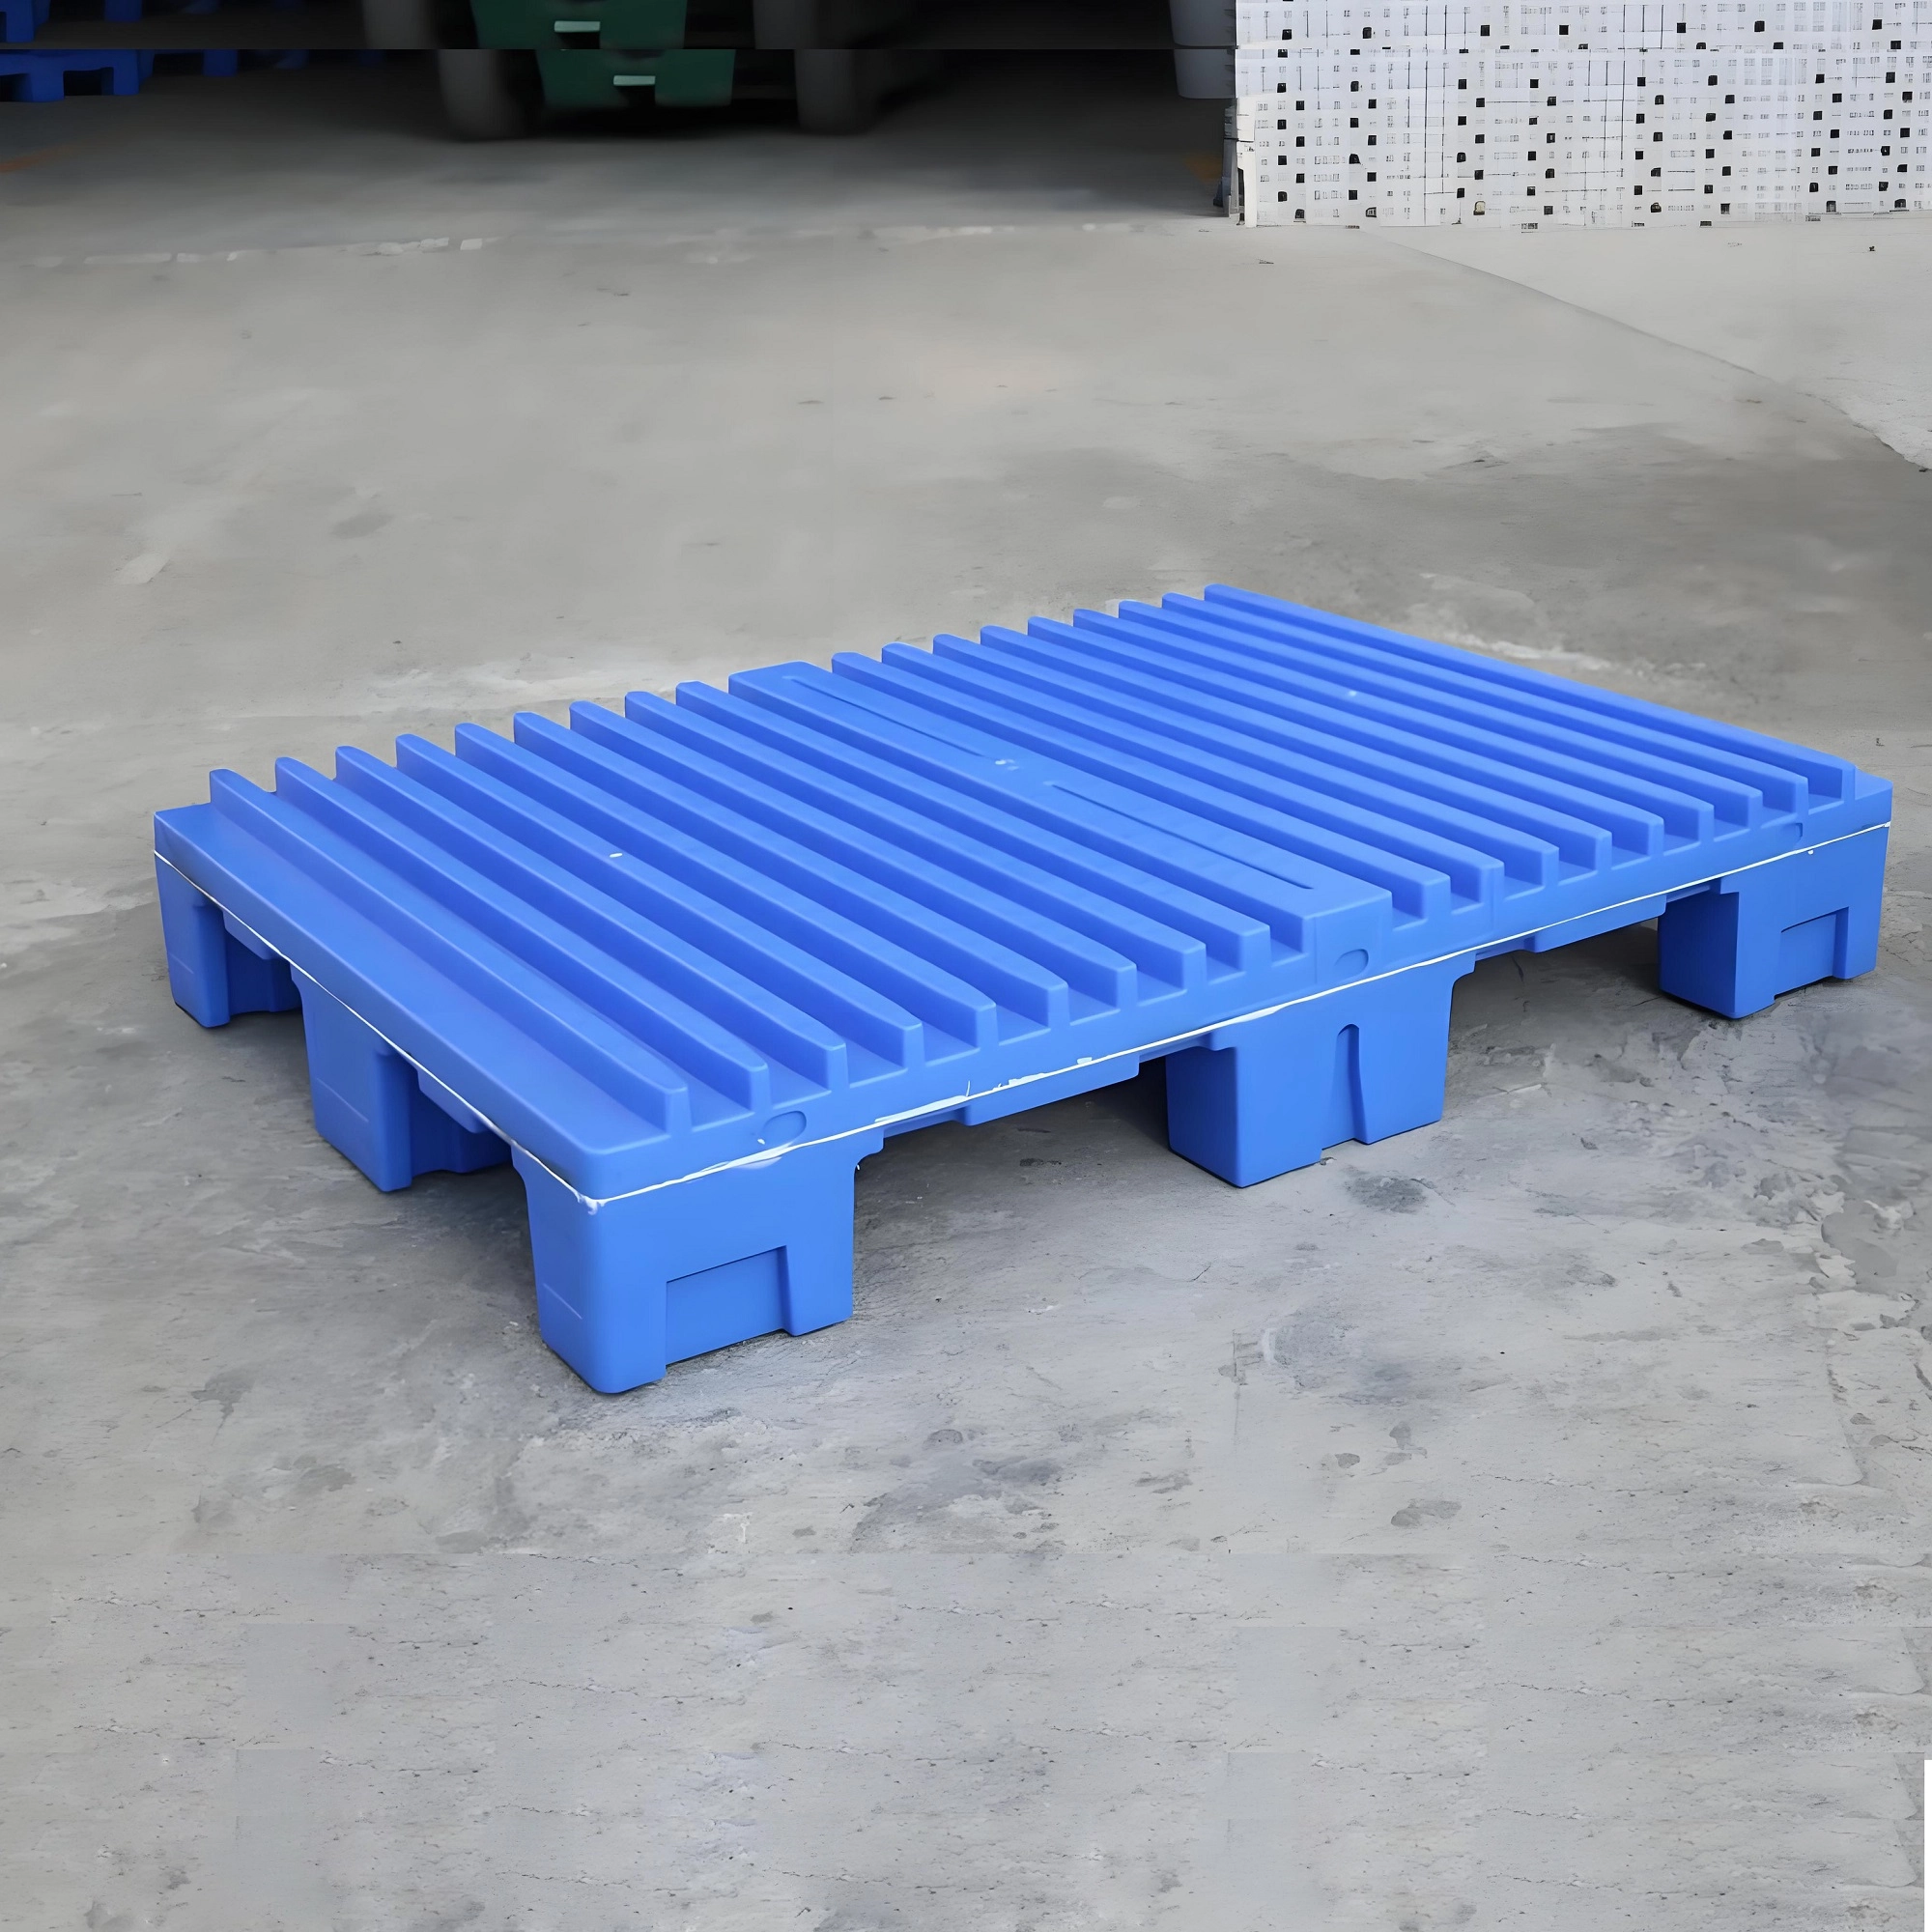
The nine-leg sing-sided printing plastic pallet is a solid and durable packaging solution designed for medium load printing and general cargo storage, and transport. It’s made of virgin HDPE or PP, featuring in robust structure, reinforced configuration with steel pipes, and a steady loading capacity.
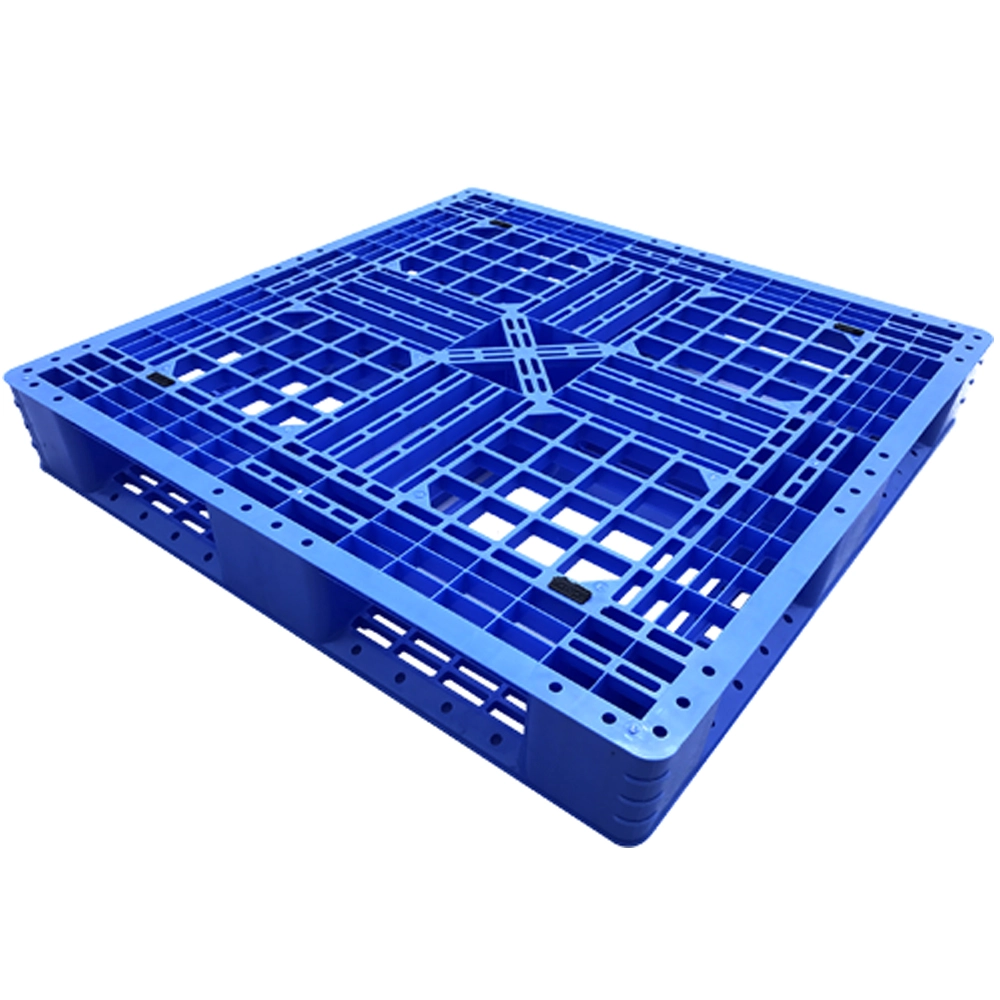
The six-runner plastic pallet, open or closed deck, is a solid and durable packaging solution designed for general and medium to heavy-duty cargo stacking, storage and transport. It’s made of virgin HDPE or PP, featuring in robust structure, a reinforced configuration with steel cores for the rack and shelf, and a steady loading capacity.

The three-runner single-sided plastic pallet is a solid and durable packaging solution designed for general and medium to heavy-duty cargo storage, transport and automated storage use. It’s made of virgin HDPE or PP, featuring in robust structure, reinforced configuration with steel cores for rack and shelf, and a steady loading capacity.
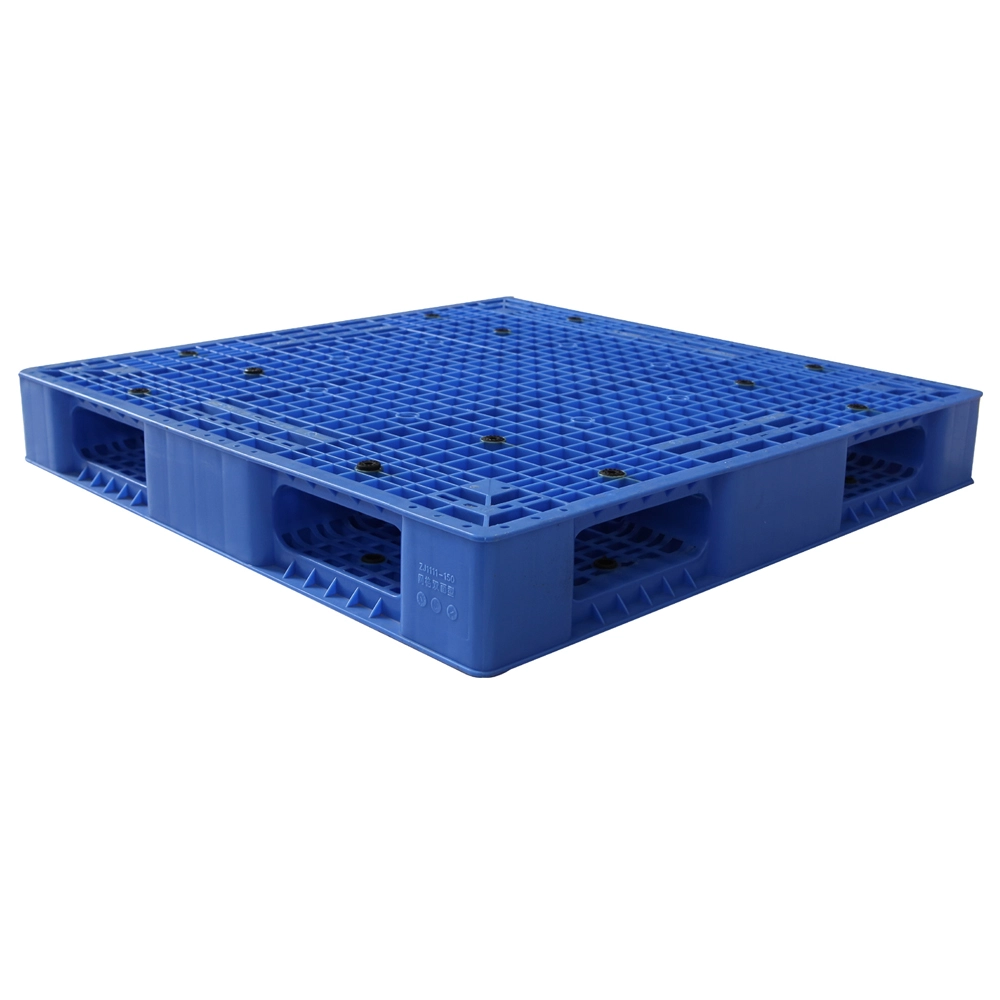
The reversible plastic pallet, open deck or closed deck, is a solid and durable packaging solution designed for general and medium to heavy-duty cargo stacking, storage and transport. It’s made of virgin HDPE or PP, featuring a robust structure, a reinforced configuration with steel cores for the rack and shelf, and a steady loading capacity for both sides.
Request More Information About Plastic Pallets
Have questions or need detailed insights on this article? Fill out the form below to contact our team for comprehensive information and support related to our plastic pallet solutions.
Contact us


+86 138 0277 8204
+86 183 4431 0917
+86 131 8916 6579

No. 15-1, Fengying Rd., Taiping Town, Conghua Dist., Guangzhou City, Guangdong Province, China.

Build the Perfect Pallet for Your Operation
Customized pallets engineered to fit your equipment, load, and workflow.
Whatsapp: +8613802778204
Scan QR Code
Guangdong Weihong Plastic Technology Co., Ltd.
Weihong
Guangdong Weihong Plastics Technology Company Ltd.